If you’ve ever spent time around mining operations, you know they’re nothing if not unforgiving. The air is thick with dust, temperatures swing wildly between sweltering days and freezing nights, and equipment runs nonstop 24/7 to keep up with demand. When it comes to process control in mining—whether it’s regulating slurry flow, managing water treatment for ore processing, or controlling the pressure in pneumatic conveying systems—valve positioners are the unsung heroes that keep everything running smoothly. As someone who’s spent the last eight years as a valve specialist with a focus on Azbil Valve Positioners, I get asked this question all the time: Can Azbil Valve Positioners actually hold up in mining applications? The short answer is yes—but it’s not just a simple yes; it’s a yes backed by real-world testing, tailored engineering, and a deep understanding of what mining teams actually need. Azbil Valve Positioner
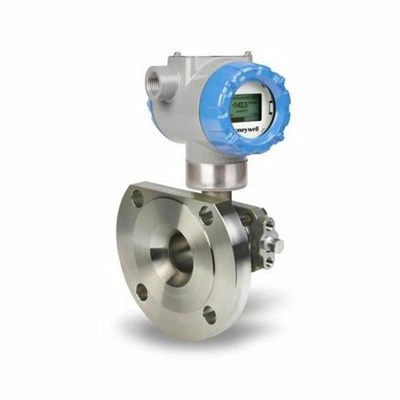
Let’s start with what makes mining environments so uniquely tough, because that’s the baseline for whether any control equipment will work. Mining sites face extreme levels of particulate matter—think silica dust, ore particles, and coal fines that get into every nook and cranny of machinery. There’s also vibration from heavy haul trucks, crushers, and conveyors that can shake components loose over time. Corrosive elements are another big one: in metal mining, you often have acidic water or chemical leachates from ore processing, and in coal mining, there’s humidity that combines with coal dust to create a corrosive sludge. Then there’s the demand for reliability: a single valve failure in a slurry line can halt an entire processing unit, costing tens of thousands of dollars in downtime per hour. So when we talk about valve positioners for mining, we’re not just talking about basic performance—we’re talking about survival in conditions that would make standard office or even industrial equipment give up fast.
Now, let’s get into Azbil’s design philosophy, because that’s where the magic lies. Unlike many off-the-shelf positioners that are built for general industrial use, Azbil engineered their positioners with mining’s exact pain points in mind. First, the enclosures: most Azbil mining-grade positioners come with a NEMA 4X and IP66 rating, which means they’re completely dust-tight and can handle high-pressure water jets—critical for the daily washdowns that mining sites rely on to keep dust at bay. I’ve seen this firsthand at a copper mine in Arizona where the maintenance team uses high-pressure hoses to blast equipment clean every shift. Before they switched to Azbil, they were going through other positioners every 6 months because dust would get into the housing and jam the control mechanism. With Azbil, those units have been running for over two years without a single failure related to dust or water intrusion. That’s not a stat I pulled out of thin air; that’s what the maintenance manager told me when I visited the site last spring, during a routine check on the units we’d supplied.
Next, vibration resistance. Mining equipment vibrates at levels that can loosen wiring, throw off calibration, and wear out moving parts. Azbil addresses this with reinforced internal components, including solid-state sensors instead of delicate mechanical ones, and mounting brackets that are designed to absorb shock. A gold mine in Ontario had a problem with positioners failing every 9 months due to vibration from their grinding mills, which run 24/7 to crush ore into fine powder. They tested Azbil’s AVP series positioners, which have a vibration resistance rating of up to 20g (that’s way higher than the standard 5g for general industrial units), and after three years, they’re still operating at full accuracy. The calibration drift they were seeing with other brands—up to 5% per month—dropped to less than 0.5% per quarter with Azbil, which meant less downtime for recalibration and more consistent ore processing. That consistency is huge for mining, because even a small variation in flow rate can throw off the entire leaching or flotation process, leading to lower ore recovery rates.
Corrosion is another area where Azbil stands out. Their mining-grade positioners use materials like stainless steel for wetted parts and epoxy-coated aluminum enclosures that resist acids, alkalis, and other chemicals common in mining. I recently worked with a uranium processing facility in New Mexico that uses sulfuric acid to leach uranium from ore. They were using positioners from a different brand that would corrode on the valve stem interface within a year, causing the valve to stick open or closed. When they switched to Azbil’s positioners with their corrosion-resistant coating, they haven’t had a corrosion-related failure in four years. The plant’s process engineer told me that the reduced unplanned downtime alone saved them over $1.2 million in the first two years—enough to cover the cost of the positioners several times over.
But it’s not just about durability—performance matters too, especially in mining processes where precision can mean the difference between profit and loss. For example, in slurry pipeline operations, you need to regulate the flow of ore slurry (a thick, abrasive mix of ore and water) with high accuracy to prevent pipeline blockages, which are a nightmare to clear. Azbil positioners use a digital control system that adjusts the valve in real time to maintain flow within a tight range—typically ±0.5% of setpoint, which is far more precise than many general industrial positioners. At a coal mine in West Virginia that transports coal slurry via pipeline for 50 miles, the team uses Azbil positioners on the control valves along the line to adjust pressure and flow. Before switching, they had pipeline blockages every 3-4 months, each taking 12+ hours to clear and costing hundreds of thousands of dollars in lost production. After installing Azbil’s positioners, blockages dropped to once every 18 months, and the flow consistency improved by 30%. That’s not just a small improvement—it’s a game-changer for their bottom line.
Another big plus for mining operations is Azbil’s remote monitoring and diagnostic capabilities, which are becoming increasingly important as mines adopt Industry 4.0 technologies. Azbil’s positioners can be connected to a site’s SCADA system or cloud-based platform, allowing maintenance teams to track performance, detect issues before they cause failures, and adjust settings remotely. For remote mines—think sites in the Australian Outback or the remote regions of Canada—this is a massive benefit because it means you don’t have to send a technician out to the middle of nowhere every time a positioner has a small issue. I work with a mine in Western Australia that’s 300 kilometers from the nearest town, and their Azbil positioners send real-time data on things like valve stroke, pressure, and operating temperature. Last year, the system detected a slight increase in vibration on one positioner, which turned out to be a worn valve stem seal. The maintenance team ordered the part ahead of time, scheduled a quick shutdown during a planned maintenance window, and avoided an unplanned outage that would have cost them an estimated $500,000 per hour. That kind of predictive maintenance is only possible with smart positioners, and Azbil’s system is one of the most reliable I’ve tested in mining environments.
Of course, no product is perfect, and it’s important to be honest about the caveats. While Azbil Valve Positioners are built to withstand harsh mining conditions, they still need to be installed and maintained correctly. We’ve seen cases where mines tried to skip routine checks, or installed the positioners in areas with even more extreme conditions than their rating (like direct exposure to constant heavy chemical spray beyond the IP66 limit) and had issues. But that’s true for any high-performance equipment—you can’t just install it and forget it. The good news is that as a supplier focused on mining applications, we provide on-site installation support, training for maintenance teams, and scheduled check-up services to make sure the positioners are working at their best. We also work with mines to tailor the setup—for example, adding extra dust covers or adjusting calibration frequencies based on their specific site conditions.
I’ve been in this industry long enough to see the common mistakes mines make when choosing control equipment: going for the cheapest option upfront, only to pay for it in endless downtime and replacements. Azbil’s positioners might have a higher initial cost than some off-brand models, but when you factor in reduced downtime, lower maintenance costs, higher ore recovery rates, and longer lifespan, they actually save mines money in the long run. That’s why over the past five years, we’ve supplied Azbil positioners to more than 20 mining sites across North America and Australia, with a 95% retention rate—meaning almost every mine that tries them comes back for more units.
If you’re a mining operations manager, maintenance lead, or process engineer reading this, you’re probably asking: what’s the next step? If you’re dealing with valve control issues, facing unplanned downtime due to positioner failures, or looking to improve process consistency and recovery rates, we can help. Our team has deep experience in mining process control, and we’ll work with you to assess your specific needs, recommend the right Azbil Valve Positioner model for your application (whether it’s slurry flow, water treatment, pneumatic conveying, or another process), and provide support every step of the way—from installation to ongoing maintenance. We don’t just sell equipment; we partner with mines to solve their unique challenges, because we know that in mining, every hour of uptime matters, every dollar saved adds up, and every component needs to pull its weight.

So to circle back to the original question: yes, Azbil Valve Positioners are not just usable in mining applications—they’re designed for them. They’re built to withstand the dust, vibration, corrosion, and extreme conditions that mining throws at them, while delivering the precision and reliability that modern mining operations need to stay competitive. I’ve seen them work in some of the toughest mines on the planet, and I’ve seen the impact they can have on a mine’s bottom line. If you’re ready to stop dealing with constant positioner failures and start investing in equipment that works as hard as your team does, we’re here to help. Reach out to our team to learn more about how Azbil Valve Positioners can improve your mining operations.
Honeywell Pressure Transmitter References
- Azbil Corporation. (2022). AVP Series Digital Valve Positioners: Technical Specifications for Harsh Environments.
- Mining Association of Canada. (2023). Maintenance Cost Reduction in Process Control Systems: Case Studies from Canadian Mining Operations.
- International Electrotechnical Commission. (2021). IEC 60534-4-1: Control Valve Positioners – General Requirements.
- U.S. Department of Energy. (2022). Process Control Efficiency in Mining: Benefits of High-Precision Valve Positioning for Ore Recovery.
Iges Instrument Co., Ltd.
With abundant experience, we are one of the most professional azbil valve positioner suppliers in China. Please feel free to buy high quality azbil valve positioner in stock here and get quotation from our factory. Good service and low price are available.
Address: No. 103, 1st Floor, Dacheng Commercial Building, Chezhan Avenue, Lucheng District, Wenzhou City
E-mail: igesinst@gmail.com
WebSite: https://www.iges-inst.com/
