Hey everyone! If you’re running a vacuum component shop or just diving into the EVA hose game, you’ve probably stared at a die for your EVA vacuum cleaner hose machine and thought—“Wait, is this the right one?” I’ve been supplying EVA vacuum hose machinery (and matching dies) for a minute now, and let’s be real: picking the wrong die isn’t just a small mistake. It’s messy, wastes material, and can set back orders so bad you’ll be fielding late-night calls from your own clients. Today, I’m breaking down exactly how we walk our buyers through selecting the right die, no fancy industry jargon that makes your eyes cross. EVA Vacuum Cleaner Hose Machine
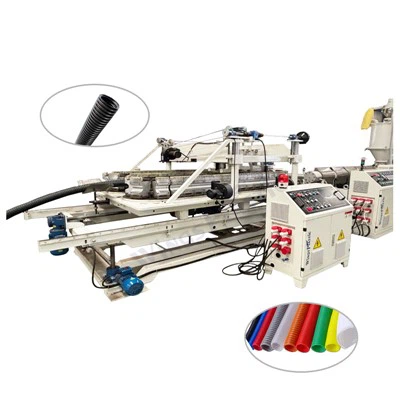
First off, let’s get one thing straight: EVA isn’t your average plastic. It’s flexible, has that soft bounce that makes vacuum hoses kink less, but it’s also sensitive to temperature and pressure when it’s melted for extrusion. A die that works for hard PVC hoses? Total garbage here. So we start with the basics that most guys skip because they’re too focused on the cool tech specs of their machine.
First question: What’s the actual hose size you’re making? I don’t mean “8-inch hose”—I mean, like, exact inner diameter (ID) and outer diameter (OD). I’ve seen people show up asking for a die that “works for any 1.5-inch hose” and wonder why their first batch comes out lumpy. EVA hoses have a pretty tight tolerance game, especially for residential vacs—you can’t have a 1.5” ID that swings to 1.58” in one spot, because it won’t fit the vacuum nozzle. Here’s the rule we swear by: measure the finished hose ID (not the one your machine’s extruding) and add 0.02 inches to that for the die’s inner bore. Wait, why? Because EVA shrinks a tiny bit when it cools down—if you make the die exactly 1.5 inches, the cooled hose will be too small to connect. For the OD? Take the finished hose’s OD, add 0.03 inches, because EVA has a bit of “swell” when it exits the die (that’s plastic 101—molten material expands a little when it’s no longer constrained). I know it’s extra math, but test this with a small pilot die first if you’re unsure—better than ruining a whole pallet of EVA pellets.
Next up: What’s the hose’s intended use? This is the part that makes all the difference between a die that lasts 6 months and one that cranks out perfect hoses for 2 years. Let’s split this into two main categories: residential vac hoses and commercial/industrial ones. Residential hoses are lightweight, flexible, and only need to handle occasional bumps around furniture. For these, we use a “standard profile die” with rounded internal angles. Sharp angles in the die can cause stress points in thin-wall EVA, which makes the hose crack after a few uses. Commercial hoses—think for construction sites, shop vacs that suck up sawdust and debris—need to be thicker, more durable, and resistant to abrasion. For those, we go with a reinforced profile die that has a slightly thicker wall in high-wear areas (the parts that rub against floors, door frames). Some buyers ask if they can just use a standard die and add extra EVA, but that throws off the hose’s balance—too thick in one spot and it kinks, too thin and it leaks air.
Wait, also—wall thickness. I can’t tell you how many times a buyer calls me panicking because their hose is either floppy (wall too thin) or stiff (wall too thick). For residential hoses, wall thickness is usually between 0.08 and 0.12 inches, commercial goes up to 0.18 inches max. The die’s wall gap is directly tied to that. If you need a 0.1-inch wall, set the die’s gap to 0.105 inches—again, that tiny extra is for that EVA swell we talked about earlier. If you skip that, your wall will be too thin and you’ll have to re-run the whole batch. It’s a small detail, but it saves hours of work.
Now, let’s talk about machine compatibility. This is another one that trips people up. Your EVA vacuum hose machine isn’t one-size-fits-all for dies. First, check the die’s connection size. Most common die sizes for small to mid-range machines are 3-inch or 4-inch flange diameters, but some heavy-duty machines take 6-inch flanges. If you order a die with a 3-inch flange for a machine that needs 4-inch, it won’t bolt on—plain and simple. I always tell buyers to send a quick pic of their machine’s die mount, or even a screenshot of the part specs from their manual, so we make sure it’s a perfect fit. No exceptions.
Then, the die’s extrusion rate. Your machine’s output (how much EVA it pushes per minute) has to match the die’s design. A die that’s made for a machine pushing 50 lbs of EVA an hour will be a total bottleneck if your machine does 100 lbs. You’ll end up with uneven hoses, and your machine might even overheat trying to force too much material through a small die. We test every die we ship with a matching extrusion rate range—usually 40-60 lbs per hour for residential, 80-120 lbs for commercial—so all you have to do is tell us your machine’s maximum output, and we’ll pick the right die for it.
Another big one: EVA grade. Not all EVA pellets are the same! Some are low-density (LD-EVA) for soft, lightweight hoses, others are high-density (HD-EVA) for heavy-duty stuff. We get a lot of buyers who say “I use standard EVA pellets” and that’s not specific enough. LD-EVA has a bigger shrinkage rate, so we add 0.03 inches to the ID of the die instead of 0.02. HD-EVA shrinks less, so stick to the 0.02 rule. If you mix up the grade, your hose will come out either too tight or too loose, no matter how perfect the other specs are. I’ve even had a buyer switch EVA grades mid-run and have to stop everything because the die was no longer working—always mention the exact EVA grade you’re using when you reach out, that’s non-negotiable.
Wait, let’s talk about long-term use too. Dies aren’t cheap, right? You don’t want to buy a new one every time you change a hose size. So if you’re a shop that might expand into different hose sizes down the line, go for a modular die. Modular dies have interchangeable inserts, so you can just swap out the inner bore and outer diameter parts instead of buying a whole new die. They cost a little more upfront, but over a year or two, you’ll save hundreds (or thousands) in replacement costs. The tradeoff? They’re not as precise as solid one-piece dies for super tight tolerance jobs, but for most small to mid-sized operations, they’re perfect.
I also need to mention something that’s not talked about enough: surface finish. The inside of the die has to be super smooth, because if there are any rough spots, molten EVA will catch and create bubbles or lumps in the hose. We use polished stainless steel for all our dies, not aluminum—aluminum wears out way faster and can leave metallic particles in the EVA, which is bad for vacuums (no one wants metal dust blowing around their house). If you see a supplier offering a cheap die with a rough surface, walk away—you’ll regret it when your first batch of hoses has holes in them.
Let’s throw in a real example to make this concrete. Last month, a guy called me from Ohio, had a small shop making residential vacuum hoses for local hardware stores. He told me he was using a die he got from a random online supplier, but his hoses were 1.47 inches ID instead of 1.5, and they kept kinking. When I asked for his specs: he wanted 1.5” ID, 2” OD, wall thickness 0.1 inches, using LD-EVA, and his machine does 50 lbs per hour. We swapped his old die for a standard profile solid die with a 1.52” ID, 2.03” OD, set for LD-EVA shrinkage, rated for 50 lbs per hour. His next batch came out perfect—no kinks, exact size, and he said his customers haven’t complained once. That’s exactly what we’re here for.
Common mistakes to avoid, by the way: Don’t guess on shrinkage rate—test it with a 6-inch test strip of EVA run through the die, measure it once it’s cooled, adjust the die size accordingly. Don’t ignore wall thickness—thin walls lead to leaks, thick walls waste material. Don’t mix die profiles for different hose types—residential dies for commercial hoses will crack in weeks. And don’t buy cheap dies to save a buck—they cost you more in wasted material and labor.
Now, let’s wrap this up. Selecting the right EVA vacuum hose machine die isn’t rocket science, but it’s not something you can wing either. You need to nail down exact ID/OD sizes, match the die profile to your hose’s use case, check machine compatibility, factor in EVA grade, and decide if a modular die makes sense for your growth.

If you’re stuck—if you have a specific hose size, EVA grade, or machine model and just want a second opinion—hit us up. We’ve been doing this for years, and we’ll walk you through every step, no pressure, no hidden fees. We don’t do one-size-fits-all dies, because every customer’s needs are different.
HDPE Pipe Machine References:
- Extrusion Dies for Plastics and Rubber, 4th Edition, C. Rauwendaal
- EVA Material Properties for Flexible Packaging and Industrial Products, Dow Chemical Company, 2021
- Vacuum Hose Manufacturing Guidelines, Industrial Plastics Association, 2022
Qingdao Wings Plastic Technology Co., Ltd.
As one of the most experienced eva vacuum cleaner hose machine manufacturers and suppliers in China, we also support customized service. Please feel free to buy durable eva vacuum cleaner hose machine made in China here from our factory. For price consultation, contact us.
Address: C02 Of Anshengyi Road, No.2 Fuan Industry Zone,Jiaodong Town, Jiaozhou City, Qingdao City, Shandong Province,China
E-mail: kelly@wingsplastic.com
WebSite: https://www.wingsextruder.com/
